
Quick Answer
A knitwear quality control SOP should verify seven connected stages: raw materials, programming and knitting, linking, washing and finishing, two-stage inspection, packing and traceability, and shipment compliance. This seven-stage framework uses checks after washing and final shaping; the order quality plan should define inspection coverage, including any 100% final workmanship check before packing. Agree fibre specifications, construction, measurement tolerances, testing methods, labels and packing requirements before production. Each checkpoint should create records linked to the actual order, so buyers can verify bulk consistency and investigate defects. Final visual inspection does not replace required laboratory testing or independent inspection.
Key Takeaways
1. A knitwear quality control SOP must begin with yarn verification and continue through shipment, not start only at final inspection. Fibre composition, yarn count, colour batch, knitting density, seam strength, washing behaviour, measurements, labels and packing accuracy can all affect whether an approved sample is repeated in bulk. A seven-step, fibre-to-garment process makes those risks visible at the stage where they can still be corrected, helping teams identify rework risks and resolve quality questions before shipment.
2. Premium knitwear requires process-specific checks because cashmere, merino wool, cotton, alpaca, viscose and blended yarns do not react identically during knitting and finishing. The same garment appearance can hide different risks in shrinkage, pilling, tension, density, colour consistency and recovery. Buyers should approve the relevant yarn, construction, washing result, measurements and hand feel before bulk production. Quality records should connect each approved requirement to an actual batch, production stage and final inspection result.
3. Two inspection stages check different conditions of the garment. The first inspection after washing identifies shrinkage, twisting, panel imbalance and surface changes before pressing. The second inspection after final shaping confirms measurements, seams, colour, labels, hangtags and packing. The agreed plan should state final inspection coverage, test methods, tolerances and acceptance criteria before production rather than after defects appear.
4. Quality control also includes traceability, packing and shipment readiness. A technically correct sweater can still create warehouse, customs or retail problems if SKU data, size ratio, barcode, care label, carton marks, packing list or shipment documents are wrong. A reliable SOP therefore closes the loop from yarn batch to final carton. For EU and US brands, these records can support material-documentation reviews and buyer compliance requests; the applicable legal obligations still need a separate market-specific review.
Table of Contents
Step 1: Raw Material Verification
Step 2: Programming and Knitting Control
Step 3: Linking and Seam Strength Control
Step 4: Washing, Fulling and Fibre Stabilisation
Step 5: Two-Stage Final Inspection
Step 6: Packing and Digital Traceability
Step 7: Logistics and Shipment Compliance
FAQ: Knitwear Quality Control SOP
Standards and Documentation
About the Author
Build a Practical QC Plan
Knitwear QC SOP Overview: 7 Steps From Yarn to Shipment
What does a complete knitwear quality control SOP cover? A documented SOP connects the approved product specification to the physical garment at every production stage. It verifies fibre authenticity, yarn specifications, knitting density, seam quality, dimensional stability, colour consistency, labels, packing and shipment documents before delivery. The table below shows the seven checkpoints in sequence. Use this knitwear quality control checklist to define the evidence each step should produce, so the factory, buyer, sourcing team or quality inspector can review it when a question arises during production or after shipment.
01
Raw material verification
02
Programming and knitting
03
Linking and assembly
04
Washing and finishing
05
Two-stage inspection
06
Packing and traceability
07
Shipment compliance
| Timeline step | Production stage | Primary quality risk | Evidence or control point |
|---|---|---|---|
| 1 | Raw material verification | Incorrect fibre, yarn count, colour batch or documentation | Yarn batch, colour reference, certificates and specification review |
| 2 | Programming and knitting | Incorrect density, tension, panel size or knitting defect | Gauge, programme, first-panel, density and measurement checks |
| 3 | Linking and assembly | Weak seams, twisting, discomfort or skipped links | Seam alignment, stretch, recovery and loose-yarn checks |
| 4 | Washing and finishing | Shrinkage, unstable hand feel or surface damage | Fibre-specific wash process, dimensions and appearance review |
| 5 | Two-stage inspection | Post-wash change, incorrect measurement or visible defect | Post-wash checks, final shaping and agreed final inspection coverage |
| 6 | Packing and traceability | SKU, label, barcode, size-ratio or carton error | Packing records, carton checks and photo documentation |
| 7 | Shipment compliance | Incorrect documents, delayed launch or receiving problem | Packing list, carton information and buyer-required documents |
Step 1 of 7: Raw Material Verification
Why does knitwear quality control start with raw material verification? Premium knitwear begins with verified yarn rather than supplier paperwork alone. Before production, the incoming yarn should be checked against the approved order specification for fibre type, yarn count, colour batch, care requirements and applicable material documents. This is particularly important for cashmere, extra-fine merino wool, cotton, alpaca, viscose blends and wool-cashmere-silk blends. Where independent verification is required for high-value fibres such as cashmere or extra-fine merino wool, select a laboratory with suitable competence and method scope, and agree specimen identification, test method and reporting requirements.
Knitwear Quality Control: Raw Material Inspection Checklist
- Confirm fibre composition, yarn count and approved yarn reference.
- Check supplier, batch, colour and dye-lot information.
- Review fibre appearance under magnification as an internal screening step.
- Review RWS, GRS, GOTS or OEKO-TEX Standard 100 documents only where relevant to the order; check the holder, validity and material or product scope.
- Identify pilling and shrinkage risks before knitting begins.
- Record any buyer-required third-party fibre or performance test.
Verification limit: Magnification is an internal screening step. It does not replace laboratory analysis when independent fibre verification is required. Define the test method, sample stage and acceptance criteria before bulk production.
Step 2 of 7: Programming and Knitting Control
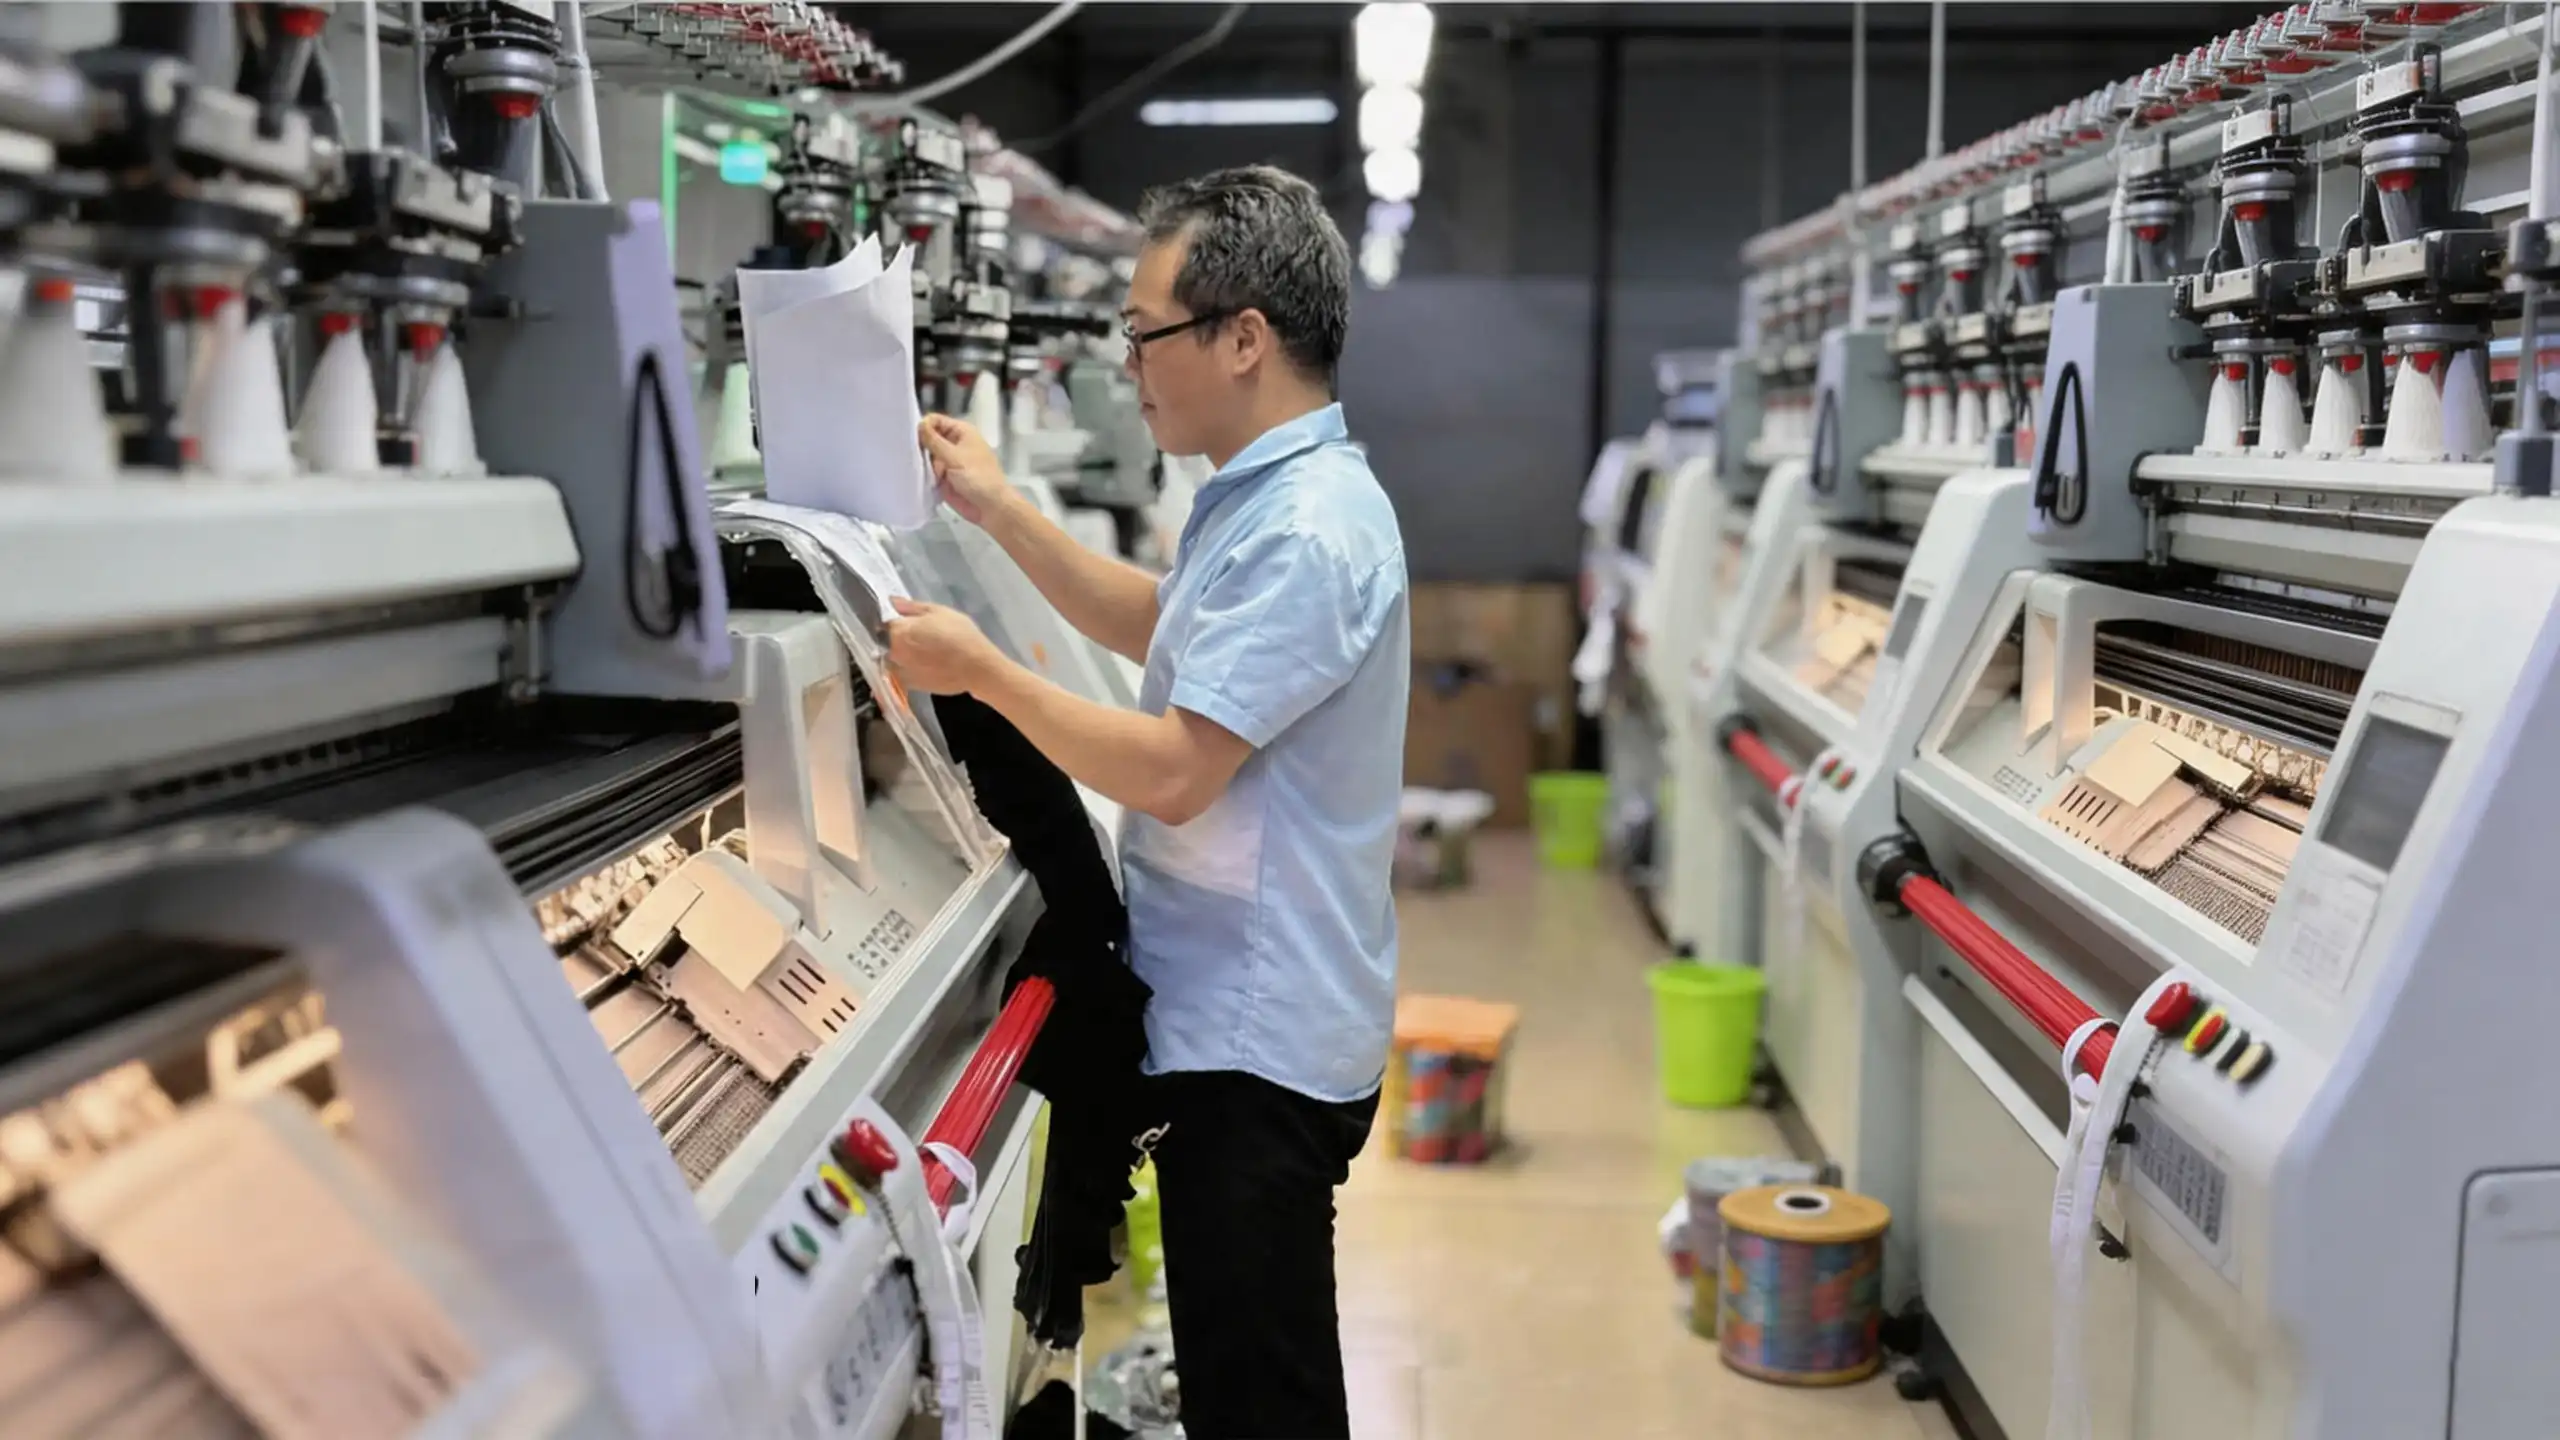
How does programming affect knitwear quality and measurement stability? Before bulk knitting, technicians calculate stitch density, needle count, panel dimensions, yarn consumption and expected shrinkage according to fibre type and garment structure. This step is important for cashmere sweaters, merino cardigans, brushed knitwear, rib structures, jacquard designs and complex blends because a visually similar panel can behave differently after washing. Computerized flat knitting technology supports repeatable tension and panel output, but production still requires in-process checks rather than waiting for the full order to finish.
Knitwear QC: Programming and Knitting Inspection Checklist
- Confirm the approved programme, gauge, yarn and construction reference.
- Review first-panel density, dimensions and visible appearance.
- Monitor yarn tension, stitch density and yarn consumption during production.
- Check for dropped stitches, holes, uneven loops and knitting marks.
- Compare panel measurements with the production specification.
- Separate clearly defective panels from accepted work in progress.
Step 3 of 7: Linking and Seam Strength Control
Why is linking quality critical for premium knitwear durability? A sweater can use the correct yarn and knitting programme but still fail through poor assembly. Linking affects seam appearance, stretch, comfort and resistance to repeated wear. The linking method and setup should suit the gauge, yarn and construction; assess the finished seam against the approved reference rather than assuming quality from the assembly method alone. Inspection should focus on shoulders, armholes, underarms, necklines, side seams, cuffs and rib-to-body connections. Stress areas require stretch and recovery checks appropriate to the garment structure before a linked garment is treated as acceptable output.
Knitwear Quality Control: Linking and Seam Inspection Checklist
- Check shoulder alignment and armhole consistency against the approved sample.
- Inspect neckline elasticity, cuff recovery and side-seam balance.
- Check for skipped links, bulky seams, twisting and loose yarn ends.
- Check underarm, neckline and cuff stretch and recovery against the approved reference; record any specified laboratory method separately.
- Separate repaired garments from accepted output for reinspection.
- Confirm that seam appearance remains clean after handling and finishing.
Step 4 of 7: Washing, Fulling and Fibre Stabilisation
Why must washing and finishing be controlled by fibre and garment structure? Washing affects hand feel, shrinkage, surface texture and final garment dimensions. Cashmere, merino wool, cotton, alpaca, mohair and viscose blends cannot be processed with one universal cycle. Water temperature, washing time, rotation speed, softener use, drying method and shaping must reflect the yarn and the buyer’s target hand feel. This stage relaxes knitting tension, stabilises dimensions and prepares the garment for accurate final shaping. For brushed cashmere, washing, brushing and steam setting also influence surface softness and pilling resistance.
Process check versus care test: A factory finishing wash is not the same as a defined domestic laundering test. For care validation, agree the wash-and-dry procedure, cycles, specimen preparation, measurement points and pass limits before testing. The standards section below identifies relevant methods; it does not certify a garment.
Knitwear QC: Washing and Finishing Inspection Checklist
- Use the approved fibre-specific washing and finishing requirement.
- Keep colours and production lots separated when required.
- Check garment measurements after washing and before final release.
- Review surface texture, softness, twisting and visible colour consistency.
- Confirm drying, steaming and shaping methods match the approved finish.
- Hold abnormal batches for review before reprocessing or packing.
Step 5 of 7: Two-Stage Final Inspection
How should two inspection stages fit the order quality plan? Knitwear changes physically after washing and pressing, so a single end-of-line inspection can miss shrinkage, twisting, panel imbalance or final measurement deviation. The first inspection occurs after washing and checks measurement change, surface condition, balance and visible defects. The second occurs after industrial pressing and final shaping, when final garment dimensions are set. Agree the final inspection coverage before production. If the plan specifies a 100% workmanship check, record completion and reinspection of repairs before packing. Keep order-specific inspection records and photos; this process control is separate from buyer acceptance sampling.
Knitwear Quality Control: Final Inspection Checklist
- Measure garments against the approved size specification and tolerance.
- Review colour under D65 lighting when the buyer requires it.
- Inspect stitches, seams, holes, stains, loose threads and yarn ends.
- Confirm finished garment balance, surface condition and shaping result.
- Verify main label, care label, hangtag and size information.
- Complete the agreed final inspection, including 100% workmanship checking where specified, and reinspect repairs before packing.
Inspection scope: A 100% final inspection does not replace specialised laboratory testing or third-party inspection required by the product, market or buyer quality manual.
Step 6 of 7: Packing and Digital Traceability
Why is packing part of a knitwear quality control SOP? Packing protects the garment, maintains brand presentation and prevents receiving errors at the buyer’s warehouse. The factory should verify SKU information, colour code, size ratio, barcode, care label, hangtag, polybag requirement and carton marks before shipment. Where recycled packaging is requested, verify the claimed recycled content and relevant supporting documents for the actual packaging supplied; do not infer a lower environmental impact from a scheme name alone. Production records can also be organised by yarn batch, production stage, inspection result, size check, packing list and shipment document to support buyer traceability requests.
Knitwear QC: Packing and Traceability Checklist
- Match SKU, colour, size, barcode, care label and hangtag to the order.
- Confirm the approved folding method, polybag requirement and carton marks.
- Check carton quantity, size ratio and packing-list consistency.
- Record packing photos when required by the buyer.
- Retain traceable links between yarn batch, inspection record and shipment.
- Confirm any recycled or lower-impact packaging claim with relevant evidence.
Step 7 of 7: Logistics and Shipment Compliance
How does quality control continue through international knitwear shipment? Quality control does not end when the garment is folded into a carton. Before shipment, carton information, packing-list accuracy, label consistency and buyer-specific documents should be checked to reduce customs, warehouse and retail-launch issues. Choose the freight route against the confirmed destination, order size, handover terms and launch schedule. Obtain a route-specific timing and cost estimate from the freight provider, including customs clearance and destination handling.
Knitwear Quality Control: Shipment Compliance Checklist
- Recheck carton marks, carton counts and packing-list accuracy before release.
- Confirm label and SKU consistency between garments, cartons and documents.
- Review buyer-required commercial, shipping and compliance documents.
- Select air, trucking or ocean freight according to order size and launch timing.
- Confirm shipment method, destination and handover requirement before dispatch.
- Retain final inspection, packing and shipment records for order follow-up.
Transit-time condition: Confirm route-specific timing with the freight provider, including customs clearance and destination handling. Production release and international delivery are separate milestones; an estimate is not a guaranteed delivery commitment.
FAQ: Knitwear Quality Control SOP
Why are two inspection stages used for knitwear?
Two inspection stages are used because knitwear can change after washing and pressing. A garment that looks correct before washing may shrink, twist, lose balance or develop a different surface appearance afterwards. The post-wash inspection identifies these issues before final pressing and shaping. Final QC then confirms measurements, seams, labels, finishing and packing after the garment reaches its intended final condition. These are process checkpoints; the buyer and factory should agree their frequency, records and release responsibility for the order.
How can a factory verify 100% cashmere or merino wool?
Verification begins with yarn supplier documents, batch information and fibre records when the yarn arrives. Internal magnification checks can provide an additional screening step, but they do not replace laboratory analysis where a buyer needs independent verification. For premium-fibre orders, agree independent testing with a laboratory competent for the selected method and specimen. A fibre-content result alone does not establish merino fineness, origin or overall garment quality. Buyers should define the required fibre-content test, method, sample stage and acceptance criteria before production begins, so results can be compared against an agreed benchmark rather than discussed after defects or discrepancies appear.
Standards and Documentation
Separate four sources of authority in the order quality plan: the factory’s internal process, the buyer’s approved specification, supplier or scheme documentation, and applicable law. A voluntary test method does not automatically become a legal requirement or establish a commercial pass level. Where ASTM, AATCC or a retailer method is specified instead, record its exact edition and do not assume that results are interchangeable with an ISO method.
AQL sampling and the lot-release decision
ISO 2859-1:2026 provides AQL-indexed acceptance sampling for inspection by attributes. It supports a decision about a lot using a sample; it does not prove that every garment conforms. Do not read an AQL value as permission to ship that percentage of defects.
Before inspection, agree the lot definition and size, random selection, inspection level, plan and inspection status, defect classes, AQL values, and acceptance/rejection numbers. Include the applicable switching rules when using the system for a continuing series of lots. An isolated shipment needs an appropriate agreed plan rather than an assumption that every continuing-lot rule fits.
Record measurements and document checks separately where their sampling differs. A factory’s 100% workmanship check and the buyer’s final random inspection serve different purposes. Neither replaces required laboratory testing. No universal AQL, measurement tolerance, shrinkage percentage or pilling grade is imposed by this guide.
Test methods and acceptance criteria
| Decision | Official method reference | What the buyer must still specify |
|---|---|---|
| Washing and drying | ISO 6330:2021 defines domestic washing and drying procedures for textile testing. | Selected procedure, machine type, detergent, load, cycles and drying route matching the intended care claim. |
| Dimensional change | ISO 5077:2007 determines dimensional change after specified washing and drying. | Specimen preparation, marking, conditioning, measurement points, results showing shrinkage or growth, and permitted changes in each direction. |
| Pilling, fuzzing and matting | ISO 12945-2:2020 uses a modified Martindale method to assess fabric surface change. | Specimen and finish, test parameters, assessment stage and agreed grade. This is not a universal garment pass grade. |
These ISO catalogue references establish method scope; they are not test reports or evidence that YouTricot has performed the tests. Agree the edition and complete instructions with the laboratory. Record the style, colour, size, production lot, sample stage, method, result and acceptance source together. An approved development sample does not establish conformity of every bulk shipment.
Safety and release limits: Identify applicable legal requirements by destination, product and intended user before production. Safety or legal failures must not be waived because a visual AQL sample passes. A supplier certificate does not automatically certify YouTricot, the finished garment or every shipment. Hold failed or ambiguous lots, document corrective action and reinspection, and record the authorised release decision.
About the Author
Frank, Founder of YouTricot. This guide is prepared with the YouTricot technical team and outlines a framework for agreeing order-specific quality controls. YouTricot Blog
Build a Practical Knitwear Quality Control Plan
Share your tech pack, target yarn, gauge, finished weight, quality tolerances, testing requirements, order quantity and target market. YouTricot can help translate this information into practical checkpoints covering material approval, sample review, bulk production, final inspection and shipment readiness.
Before you start development, read these guides:
Related Cashmere Sourcing Guide
If you are sourcing premium cashmere knitwear for Poland or the wider EU market, this guide covers cashmere quality verification, supplier evaluation, MOQ planning from 50 pieces per style per colour where the yarn, colour, structure, trims, testing, finishing and technical route are feasible, OEM/ODM production, EU compliance, customs and shipping.
How Should Brands Verify Machine-Washable Merino Wool Claims?
The quality control process above shows the role of washing and post-wash inspection in knitwear production. For merino wool sweaters, the final care solution also depends on specific yarn treatment, gauge, stitch structure, seam method, trims, colourway, finishing process and the full wash-and-dry cycle. The next guide explains how to connect these variables to repeatable test protocols and evidence-based care labelling.
Further Reading
YouTricot Guide
Kids Knitwear Manufacturer Guide: Safety, Sizing and Durability
For a custom kids sweater quality control checklist, add the intended age group, target market, trim and attachment risks, care validation and the applicable safety review to the order brief. The linked children’s knitwear guide covers the product-specific decisions beyond this general SOP.
Read the full guide here : kids knitwear manufacturer